MAIN MENU

As production cycles become shorter, dynamic weighing performance depends on more than load cell accuracy. Measurement repeatability, mechanical integration, signal processing and response time all determine whether reliable weight information is available in time to support machine control. For engineers designing high-speed weighing, filling and dosing systems, these parameters increasingly need to be considered as part of the same measurement chain.

Shorter measurement windows

For machine builders, increasing throughput creates a fundamental constraint: the faster the production cycle, the less time there is to establish a reliable weight measurement.

Under real production conditions, the weight signal is rarely stable. Conveyor and actuator vibration can excite the weighing structure. Product handling introduces impacts and parasitic forces. In filling and dosing applications, turbulence, foaming and changing flow behaviour and machine rotation create additional transient effects.

None of these phenomena is new. What changes at higher production speeds is the time available to deal with them.

As cycle times decrease, the weighing system has less opportunity to settle before the measurement must be evaluated and the machine must make its next decision.

The key question is no longer how quickly a measurement can be taken.

It is whether sufficiently reliable weight information can be extracted from the available measurement window. For high-speed dynamic weighing, increasing the sampling rate does not solve the problem if the resulting information cannot be evaluated reliably within the machine cycle.

Machine conditionEffect on weighingEngineering requirement
Shorter cycle timeSmaller measurement windowObtain a usable measurement faster
Reduced settling timeGreater influence of transient effectsIncrease sensor dynamic response
Higher operating speedGreater influence of dynamic disturbancesSeparate useful weight information from disturbances
Earlier control decisionsLess time for signal processingControl measurement and processing latency
Tighter process tolerancesGreater impact of cycle-to-cycle variationMaintain stable process performance

Accuracy and dynamic performance

Load cell accuracy remains fundamental, but it describes only one aspect of the performance of a complete weighing system.

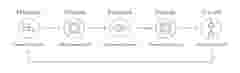
Between the physical load and the machine’s response sits an entire measurement chain:

image

Each stage can influence the result. Mechanical compliance affects settling behaviour. Incorrect load introduction, side loads and parasitic forces can distort the measurement. Signal processing can improve disturbance rejection but also affect response time. Communication and controlsystem latency determine when the machine ultimately reacts.

For machine designers, several performance characteristics therefore need to be consideredindividually.

A load cell with excellent accuracy specifications can therefore still be part of a system that performs poorly once installed in a dynamic machine.

Conversely, appropriate mechanical integration, sensor selection and signal processing can help the  measurement chain deliver repeatable results under demanding production conditions.

For OEMs, this shifts the focus from the accuracy of an individual component towards a broader requirement: delivering reliable and repeatable measurement within the time available on the machine.

ParameterEngineering significance
AccuracyCloseness of the measurement to the reference value
RepeatabilityConsistency of repeated measurements under the same conditions
Dynamic performanceReliability of the measurement while loads and disturbances are changing
Process capabilityAbility of the production process to remain consistently within specified limits

Signal processing and response time

Signal processing is central to dynamic weighing. A weighing signal can contain unwanted components generated by mechanical vibration, product handling and transient process effects. Digital filtering can attenuate these disturbances and make the weight information easier to evaluate.

But filtering creates an important engineering trade-off: signal stability versus response time.

Consider a filling process:

image

If processing delays the information excessively, the physical process continues while the control system is still determining the appropriate response. As a result, a highly stable measurement may become available too late to support the optimum control decision.

The objective is not to minimise filtering. Effective digital filtering is essential in many dynamic applications. Instead, the processing strategy must reflect the disturbance spectrum, machine dynamics and available measurement window.

Targeted filters can attenuate disturbances at known frequencies. Triggering can define when and under what conditions measurement data is evaluated. Sampling and processing parameters can then be adapted to the dynamics of the application.


The  optimisation challenge therefore involves balancing:

  • Disturbance rejection
  • Repeatability
  • Response time


In dynamic weighing, the most useful signal is not necessarily the smoothest. It is the one that provides sufficiently reliable information within the time availablefor action.

image

Optimise Dynamic Filling Performance

Explore the key engineering factors behind filling accuracy, repeatability and throughput, with practical guidance on measurement architecture, signal response and real-time control.

Dynamic weight signals as process information

Weight is often treated primarily as an end result. In dynamic checkweighing, for example, a weight value can be used to determine whether a product remains within specified limits: Measure ➔ Weight value ➔ Accept / Reject

But the signal generated during a dynamic weighing operation evolves over time. This time-dependent behaviour can contain information beyond the final weight value.

In a filling application, the signal can show progression towards the target weight, transitions between filling phases and settling behaviour after cut-off. Comparing successive cycles can also reveal changes in process behaviour.

This information needs to be interpreted carefully. A load cell does not directly measure viscosity, foaming or machine vibration. It measures the mechanical load transmitted through the weighing structure. However, changes inthe signal, evaluated in the context of the machine and its operating state, can provide  insight into the physical process.

This creates two complementary uses for weight measurement:

Weight verificationProcess measurement
Final weightTime-dependent weight signal, reference of next filling cycle
Accept rejectProcess behaviour
End-result verificationInformation duringoperation
Detect non-conforming productDetect process variation
Quality-control inputPotential processcontrol input

The final weight describes the outcome of an operation. The evolution of the weight signal can provide additional information about the process that produced that outcome.

This extends weighing beyond inspection towards its use as a process measurement tool.

Weight measurement in control loop

Process information becomes particularly valuable when it is available while the physical process can still be influenced. Filling provides a straightforward example.

Continuous weight acquisition can be used to evaluate filling progress and control transitions between: Course fill > Fine fill > Cut-off

Instead of measuring only the final result, weight becomes one of the variables used by the machine during the filling operation. 

This also provides a more precise definition of real-time weighing. A high sampling rate or fast communication interface alone does not enable real-time process control.

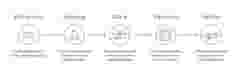
Several stages contribute to the time between a physical change and the machine’s response: Sensor response > A/D conversion > Signal processing > Communication > Control execution > Actuator response

The measurement must therefore be both reliable enough and available early enough to influence the process within the required control window.

When these conditions are met, real-time weight data can become an active input to closed-loop process control.

Repeatability and process variation

The relationship between measurement performance and production efficiency is particularly visible in filling and dosing applications.

A process must avoid underfill while also limiting unnecessary overfill. If cycle-to-cycle variation is high, moving closer to the target weight can increase the likelihood of producing units outside the required limits. 

Reducing variation is therefore as important as improving an individual accuracy specification.

The relationship can be considered as a sequence: 

1. Consistent control decision

2. Repeatable cut-off

3. Reduced process variation

4. Tighter target-weight control

5. Lower product giveaway and fewer rejects

For machine builders, this connects measurement repeatability directly to target-weight optimisation, yield and process efficiency.

The engineering objective is therefore not simply to generate a more precise weight value. It is to maintain predictable measurement and control behaviour  from cycle after cycle under real production conditions.

Measurement architecture for dynamic applications

Once weight measurement becomes part of the control loop, the architecture of the weighing system becomes increasingly important.

Signal acquisition, filtering, weighing algorithms, diagnostics and communication do not necessarily have to reside within the same component. Depending on the application, these functions may be distributed across the load cell, weighing electronics, an edge device and the machine controller.

The choice depends on measurement speed, required repeatability, machine mechanics, number of channels, control-loop requirements and industrial communication needs. The objective is to reduce the path between:

image

This is where Dynamic Weighing 4.0 becomes into its own. It is not simply about digitising a load cell or generating more weighing data. The goal is to provide reliable measurement information available where and when the machine can use it.

Five Questions with Mark Gao, Product Manager at HBK

We spoke with Mark Gao, Digital Load Cell Manager Product Manager at HBK, about the practical implications for machine builders and the measurement architectures available for high-speed dynamic weighing.

The starting point should always be the application rather than an individual load cell specification. We need to understand the capacity and required accuracy, but also the cycle time, available measurement window, mechanical load introduction, expected disturbances and the point at which the machine needs the measurement result.

For dynamic applications, these parameters are closely connected. If the mechanical system requires a long time to settle, simply selecting a faster sensor will not necessarily solve the problem. Equally, very aggressive filtering may produce a stable signal but make the result available too late.

This is why we look at the complete measurement chain. The sensor, mechanical integration, signal processing and control requirements need to be considered together. The optimum solution depends on what the machine needs to achieve within each cycle.

The first step is to understand the source and characteristics of the disturbances rather than treating all signal variation as generic noise.

Machine vibration, for example, may occur within identifiable frequency ranges. In that case, appropriate digital filtering can suppress specific disturbances while preserving the dynamic information required for the measurement. Triggering is also important because it allows the measurement to be evaluated at the appropriate point in the machine cycle.

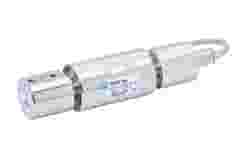
Digital load cells such as FIT7A are useful in this type of architecture because sensing and digital signal processing are closely integrated. Filtering and triggering functions can be configured around the dynamic behaviour of the application.

The objective is not simply to obtain the smoothest possible signal. It is to achieve the repeatability required by the process with a response time compatible with the machine cycle.

Once the weight value is required during the process rather than only at the end, the measurement system becomes part of the machine’s control architecture.

Filling is a good example. The system may need to evaluate weight continuously, control transitions between coarse and fine filling, and determine the cut-off point. The shorter the path between measurement, evaluation and action, the more effectively the weight information can be used for process control.

This is where an integrated digital solution such as FIT5X becomes relevant. Measurement, digital processing and functions for filling, dosing and checkweighing can be located close to the measurement point. The digital outputs of FIT5X can also control a flow valve directly, alongside the interfaces needed to communicate with the machine.

For an OEM, the benefit is not simply that the sensor is digital. The important point is that measurement information and weighing functionality can be integrated more directly into the machine architecture.

There is no single architecture that is right for every application.

An integrated digital load cell can be very effective when machine builders want a compact, standardised measurement solution. Other machines require greater flexibility in sensor selection, channel configuration, processing or communication.

In those cases, separating the sensing element from the processing layer can be advantageous. A load cell such as PW25, for example, can be combined with digiBOX Weighing, bringing signal processing, real-time data handling, diagnostics and industrial communication closer to the process while retaining flexibility at sensor level. 

This also allows machine builders to decide where different functions should reside. Some processing can take place close to the physical measurement, while the PLC remains responsible for the wider machinecontrol sequence and higher-level systems use the resulting information for monitoring or analysis.

The architecture should therefore be selected according to the measurement and control requirements of the machine, rather than a predetermined view of where weighing intelligence should be located.

I think the largest gains will come from treating measurement as part of the complete machine system rather than optimising individual components in isolation.

Sensor performance will continue to improve, but there is also significant potential in mechanical integration, digital signal processing and the way measurement information is used by the control system.

Moving appropriate processing closer to the measurement point can make information available sooner. Improved connectivity can make the same measurement information available for control, diagnostics, and process monitoring. Analysing measurement behaviour across multiple cycles can also provide a better understanding of process variation than relying solely  on final weight values.

For machine builders, the opportunity is to use weighing not only to determine whether a product meets a weight requirement, but also to make the process itself more observable and controllable.

That is where we see dynamic weighing developing: combining reliable  measurement with the processing and system architecture needed to provide useful information at the right point in the machine cycle.

Related content